
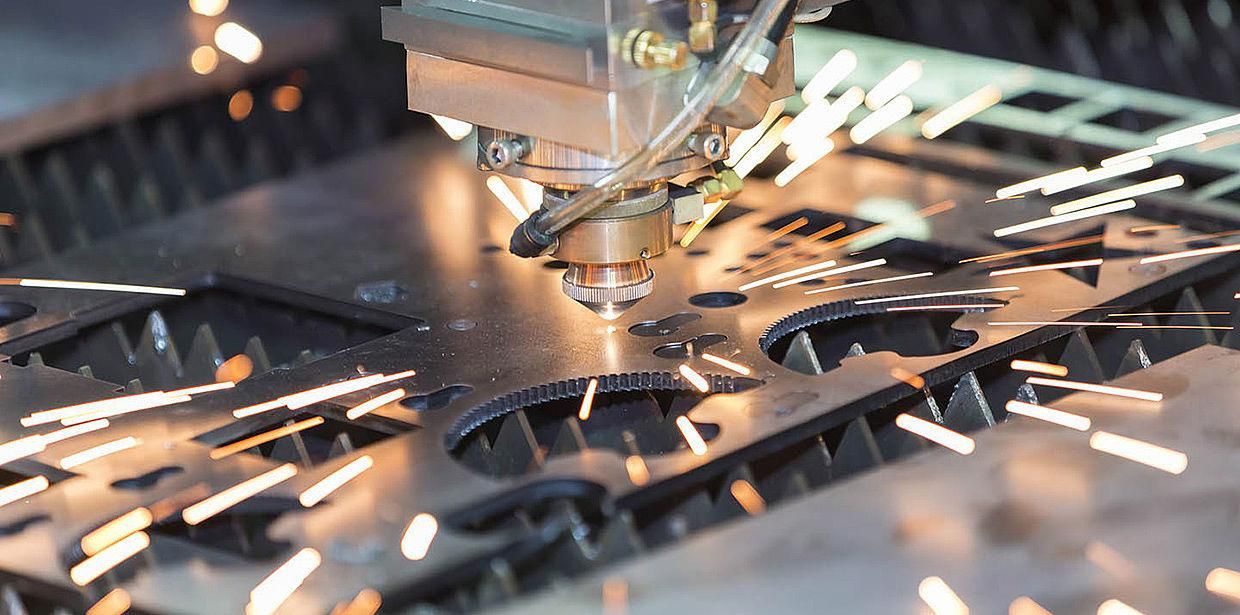
Laser, plasma & oxy-fuel cutting
Laser, plasma and oxy-fuel cutting in one group, from thin sheet to heavy plate. Your blanks are cut by the supplier that also bends, welds and paints them, so there is no separate cutting subcontractor to qualify.
Laser cutting
Fiber and CO2 lasers
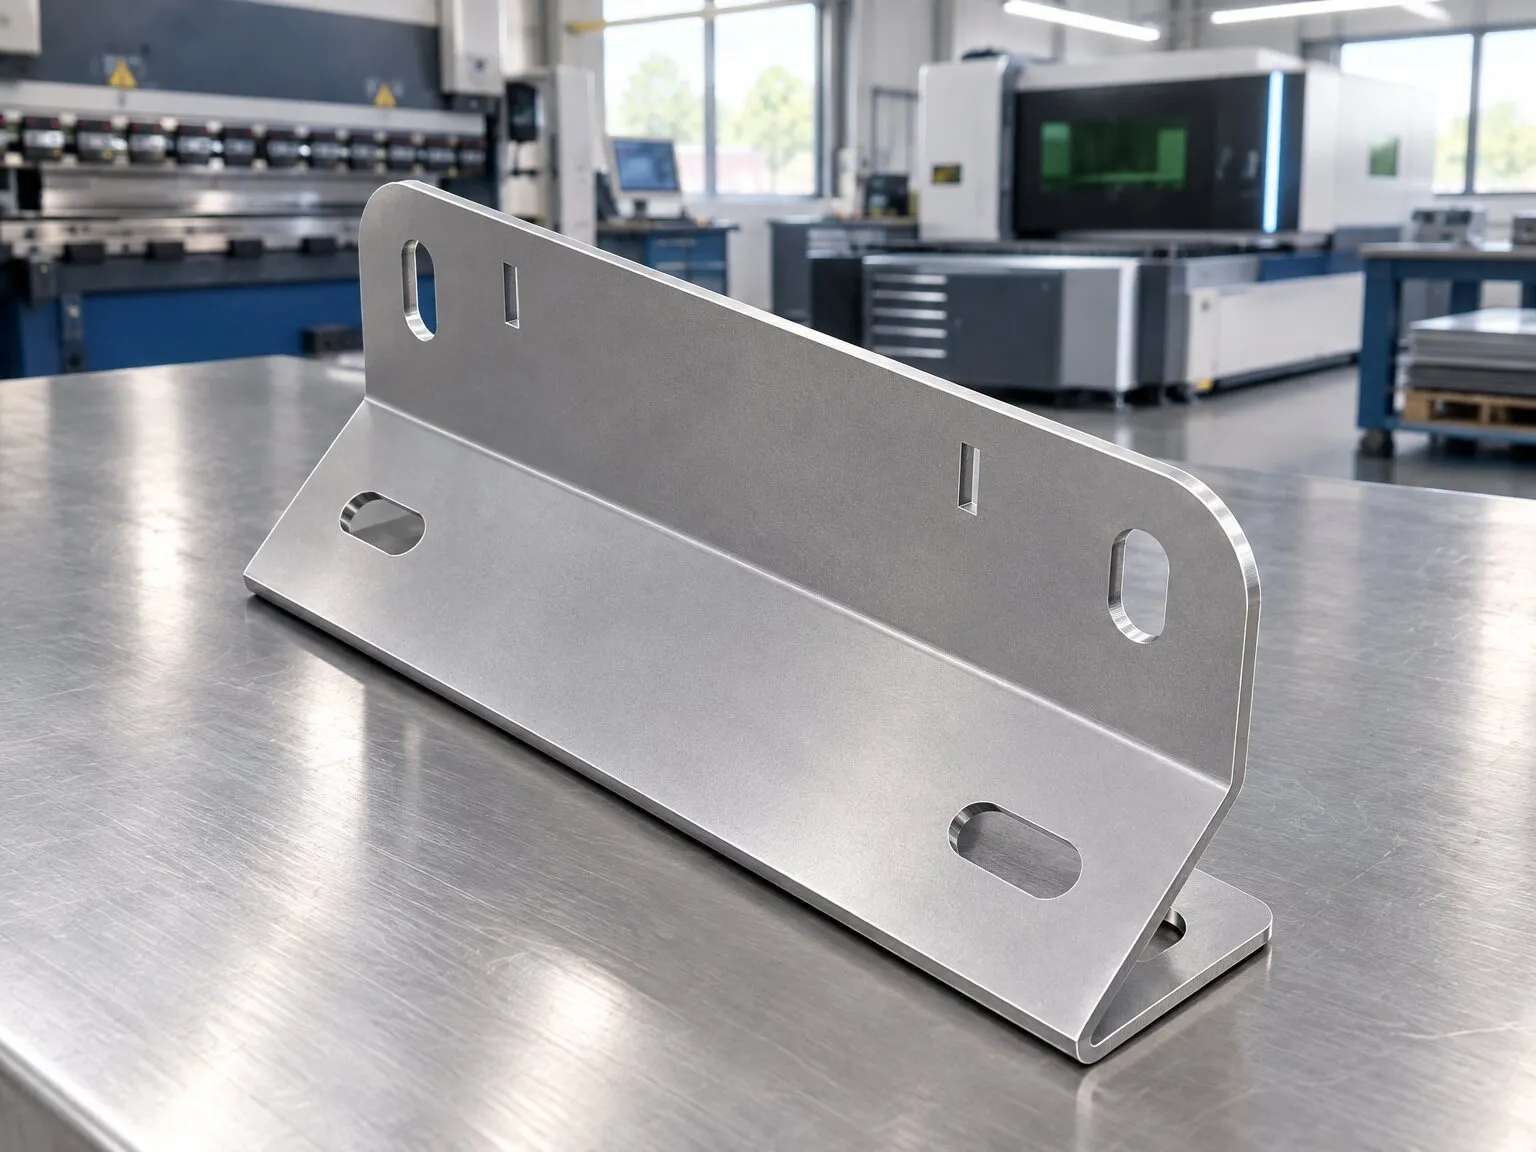
The laser cuts your sheet parts that go on to bending, welding and painting.


- Feature
3 fiber lasers: 1 × 3000 × 1500 mm, 2 × 6000 × 2500 mm
BenefitSheet parts in series are cut with clean, bright edges, ready for the press brake.
- Feature
3 CO2 lasers: 2 × 4000 × 2000 mm, 1 × 6000 × 2500 mm
BenefitA second laser technology in the same thickness range, on the same sheet formats.
- Feature
Sheets up to 6000 × 2500 mm
BenefitLong blanks are cut in one piece, with no joint to weld, and large sheets nest more parts with less scrap.
Proof6000 × 2500 mm
- Feature
Up to 20 mm thick
BenefitThicker parts of the same order move to plasma or oxy-fuel in-house: the whole cut list stays with one supplier.
Proof20 mm laser · 40 mm plasma
Oxy-fuel cutting
XXL formats for heavy plate
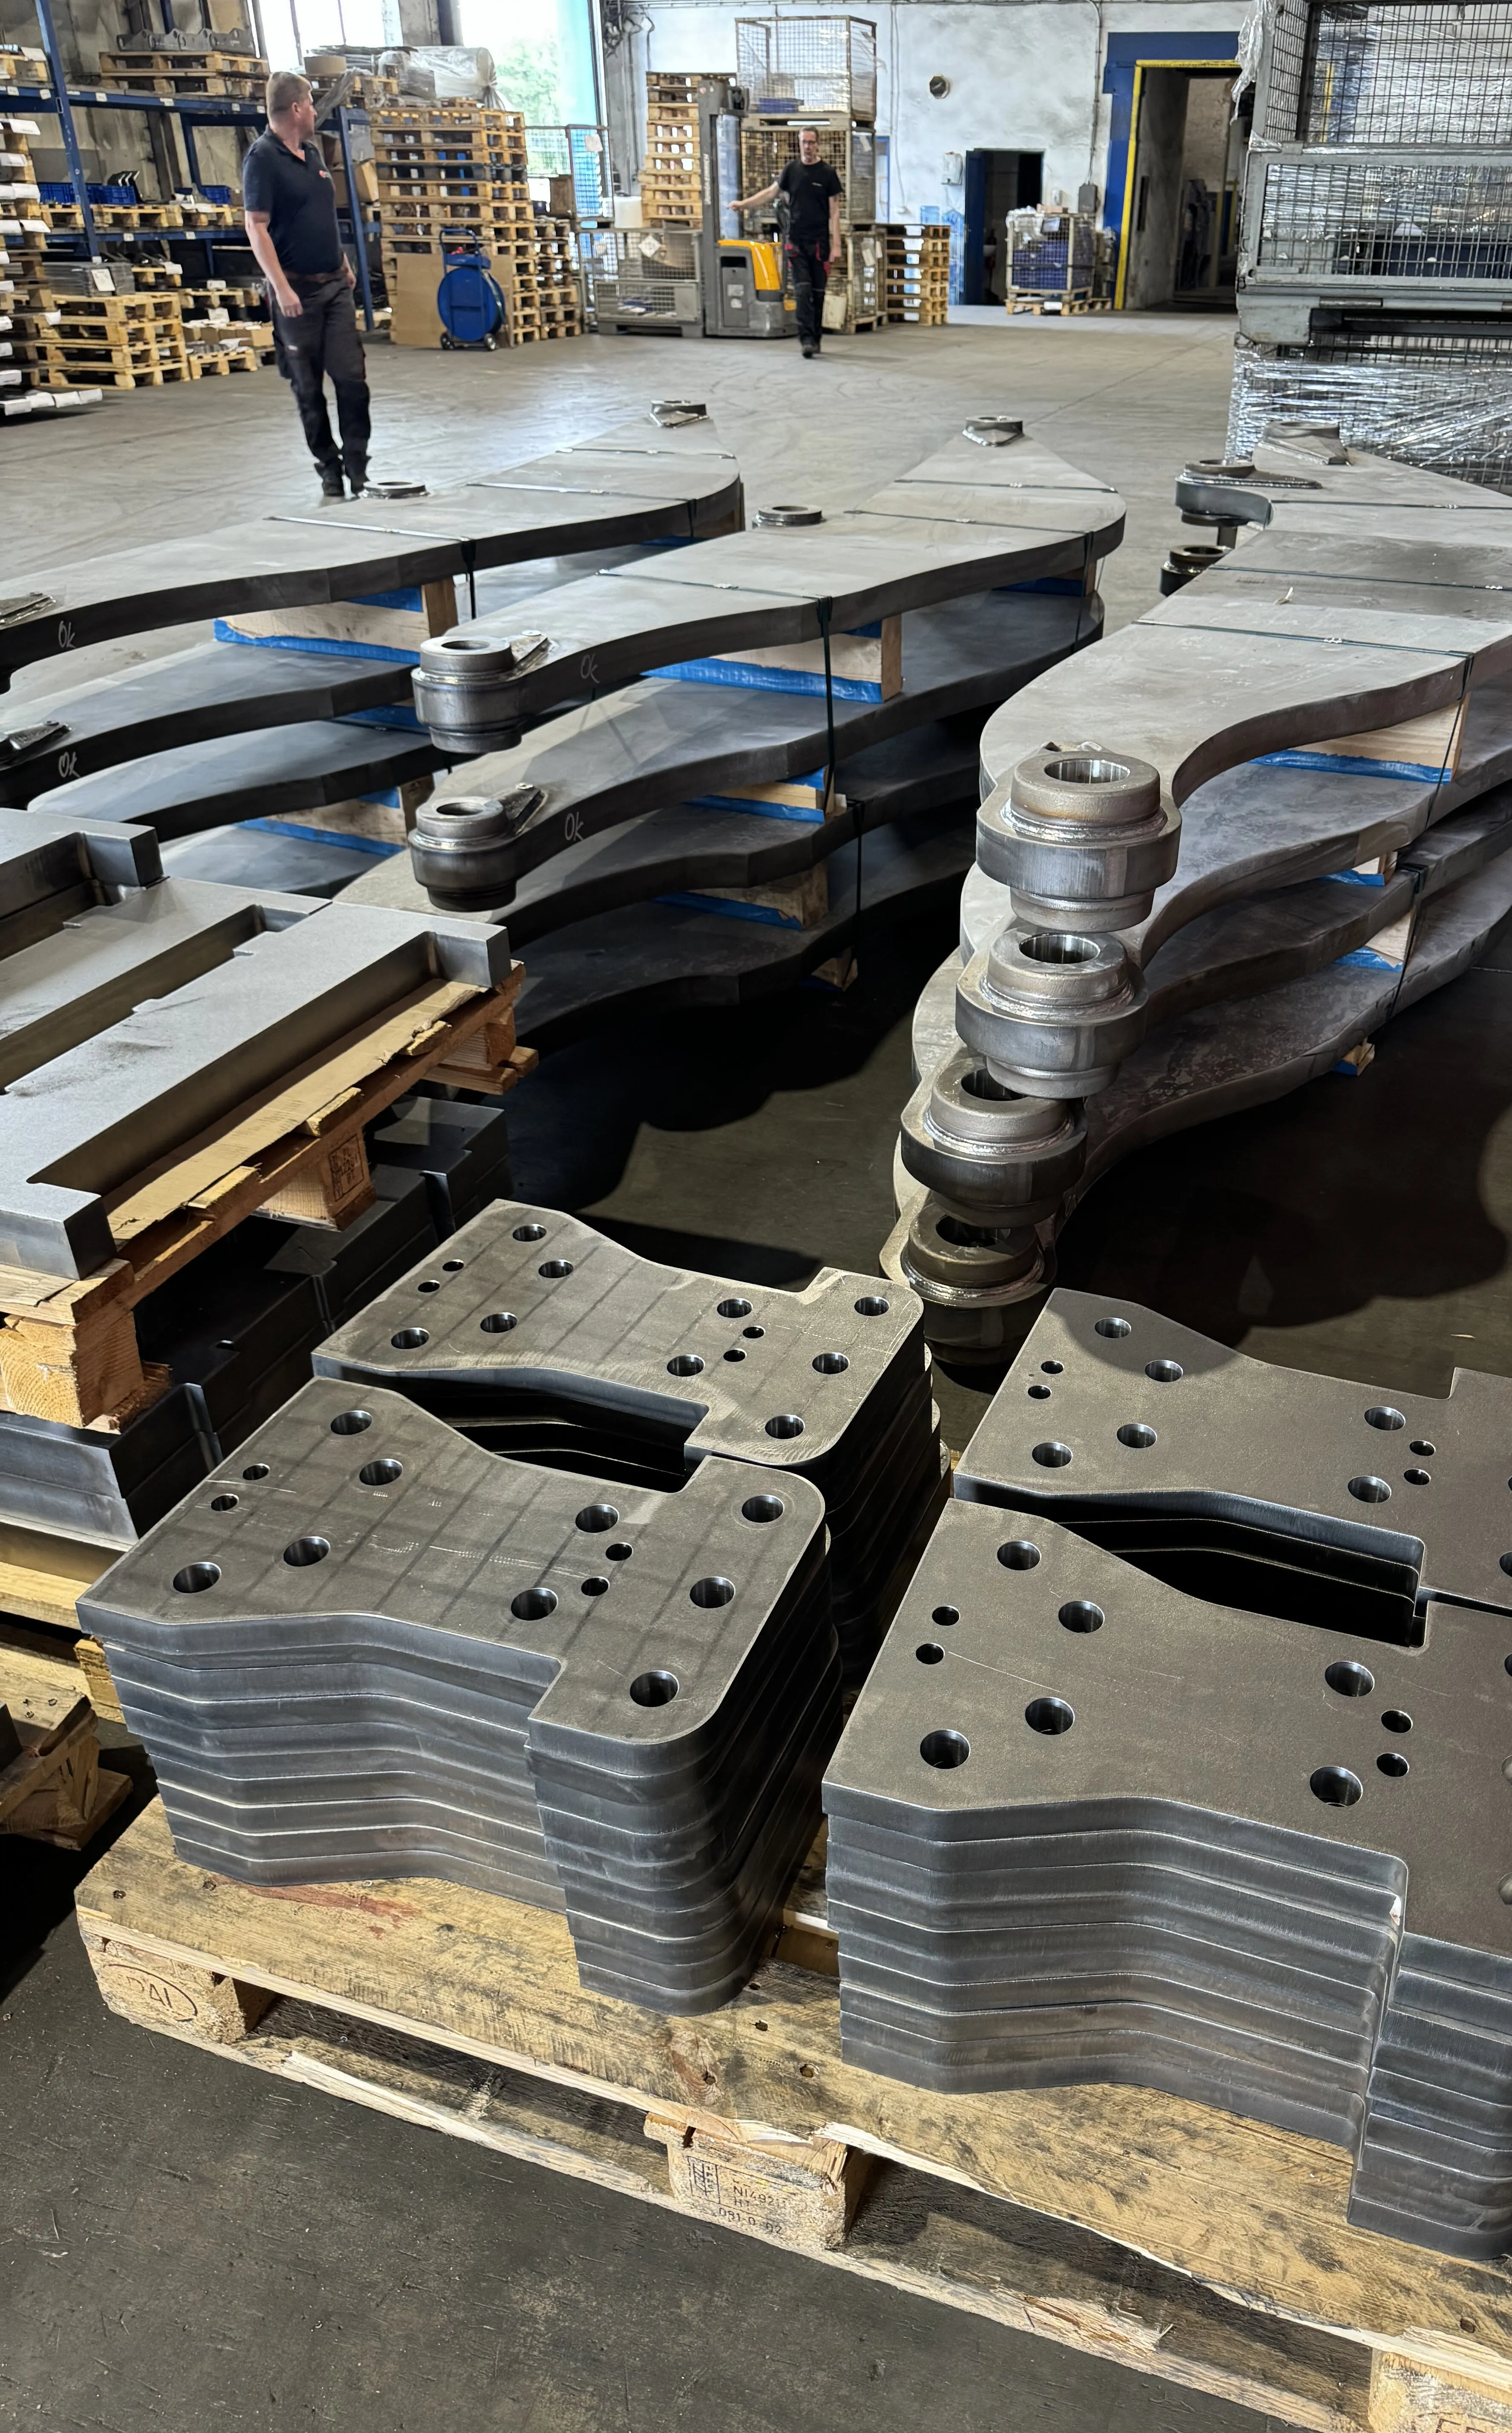
Oxy-fuel takes the plate that is too thick for laser and plasma.


- Feature
Plate up to 300 mm thick
BenefitThe heavy plate parts of your assembly come from the same supplier as its sheet parts.
Proof300 mm
- Feature
Table up to 12000 × 5000 mm
BenefitLarge plate parts are cut in one piece instead of being split and welded back together.
Proof12 × 5 m
- Feature
Up to 10 torches cutting at once
BenefitIdentical parts are cut in parallel, which keeps the cost per part down on repeat series.
Proof10 torches
Plasma cutting
Medium-thick plate up to 40 mm
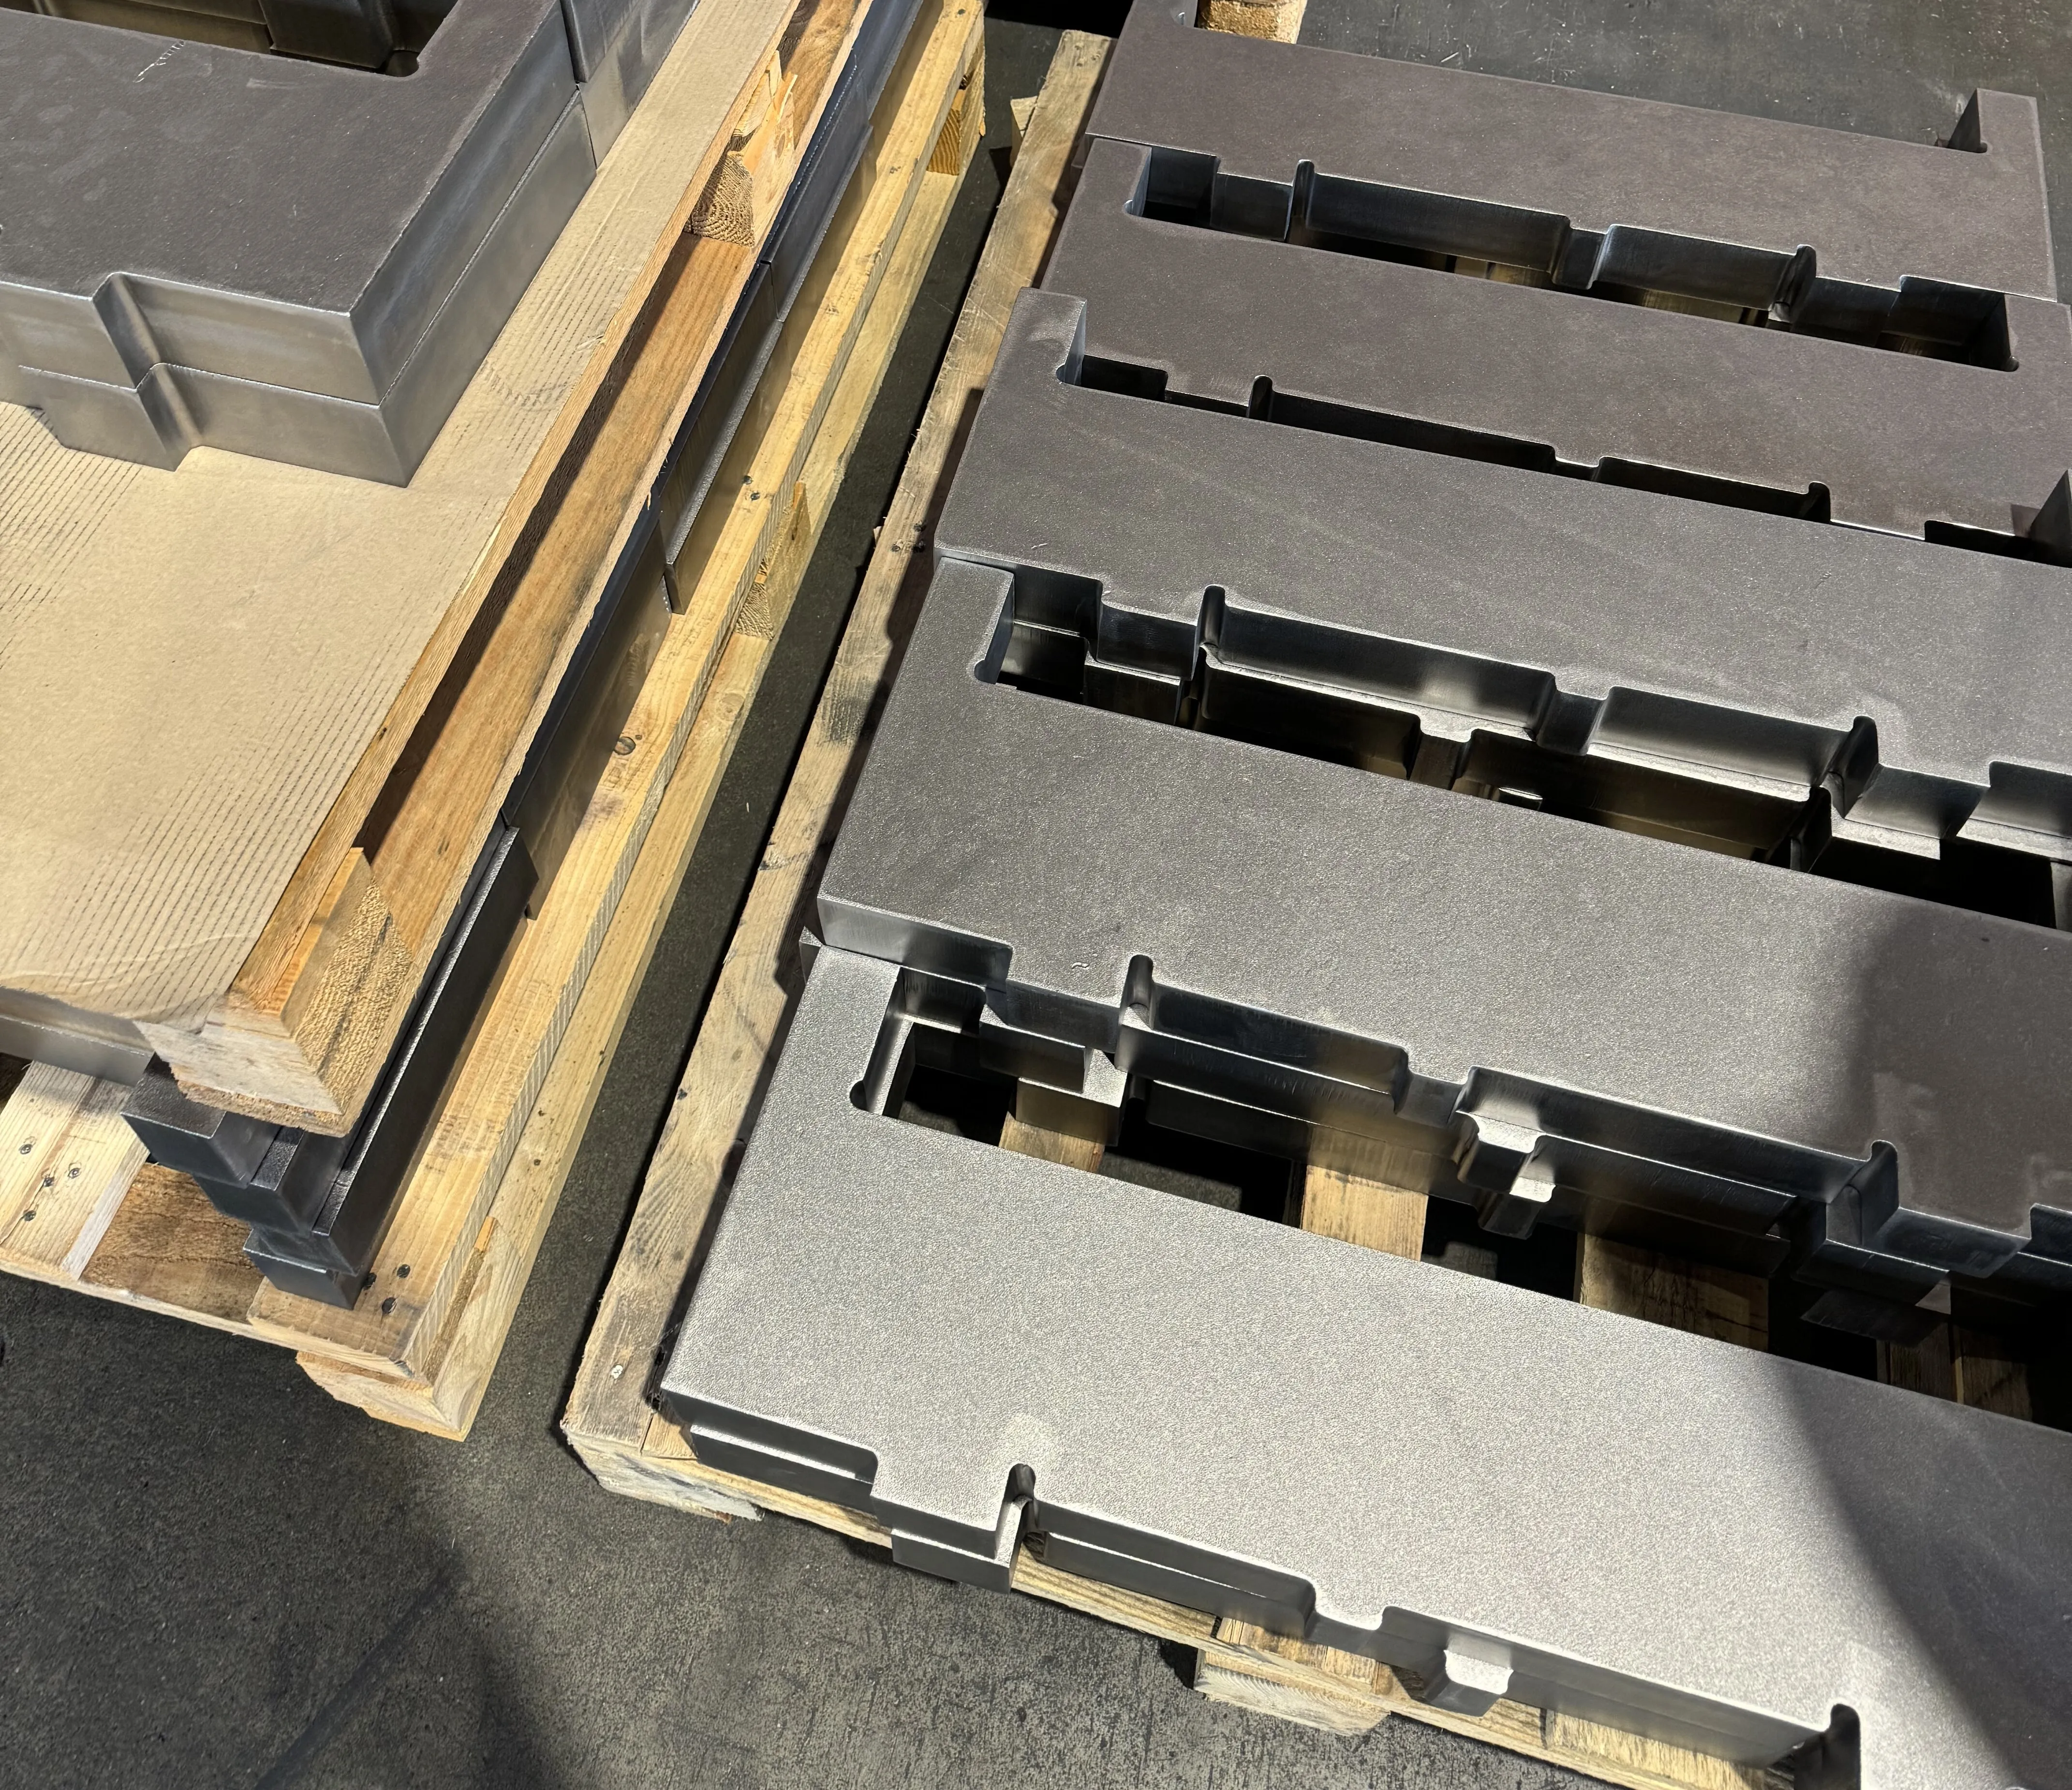
Plasma covers medium-thick plate, between the laser and oxy-fuel ranges.


- Feature
Plate up to 40 mm thick
BenefitThe cut edge is ready for welding, so parts go straight to the welding line.
- Feature
Same XXL table, up to 12000 × 5000 mm
BenefitLarge medium-thick parts are cut in one piece, without a joint.
Proof12 × 5 m
- Feature
2 torches cutting at once
BenefitSeries parts are cut two at a time, which shortens machine time per part.
Proof2 torches
Frequently asked questions
What is the maximum thickness you can laser cut?
Up to 20 mm, on sheets up to 6000 × 2500 mm. Thicker plate goes to plasma (up to 40 mm) or oxy-fuel (up to 300 mm) in-house, so the whole cut list stays with us.
Which laser machines do you run?
Six lasers: three fiber lasers (one 3000 × 1500 mm, two 6000 × 2500 mm) and three CO2 lasers (two 4000 × 2000 mm, one 6000 × 2500 mm).
How thick and how large can you oxy-fuel cut?
Up to 300 mm thick, on formats up to 12000 × 5000 mm, with up to 10 torches cutting at once. Large plate parts are cut in one piece and identical parts in parallel.
When do you use plasma cutting?
For medium-thick plate up to 40 mm, on the same 12000 × 5000 mm table with two torches. The cut edge is ready for welding.